800.942.4447

 Addresses
 Wallet
 Orders
 Invoices
 Item History
 Favorites
 Change Password
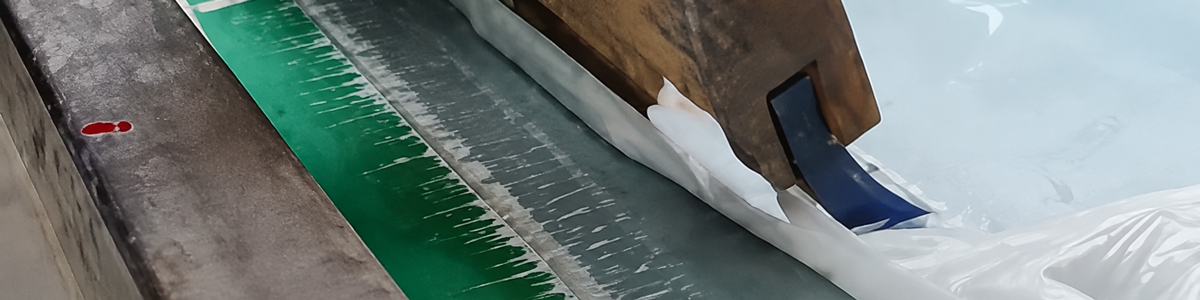
Properly preparing screen printing ink can make the difference between a smooth production run and hours of unnecessary adjustments. Ink that has been sitting may feel stiff, separated, or difficult to move, but that does not automatically mean it needs reducer or has gone bad.
The correct consistency depends on the ink, garment, mesh count, artwork, and desired deposit. A high-opacity white should not feel exactly like a process color, and glitter ink should not behave like a general-purpose plastisol. The goal is not to make every ink thin. The goal is to prepare each ink so it performs the way it was formulated to perform.
For plastisol ink, the proper sequence is simple: bring it to room temperature, mix it thoroughly, test it through the production screen, and only then decide whether an approved reducer is necessary.
What Does Ink Consistency Mean?
Printers often use the words consistency and viscosity interchangeably. They are closely related, but they are not exactly the same.
Viscosity describes how strongly a liquid resists flowing. A higher-viscosity ink generally feels thicker, while a lower-viscosity ink flows more easily. Consistency is the broader way the ink behaves, including whether it is smooth, uniform, separated, lumpy, stringy, creamy, or contaminated.
An ink may seem thick while sitting in the container but become much easier to print after mixing. It may also have the correct viscosity but still require mixing because pigments or specialty particles have settled.
The correct ink should:
- Flood the screen evenly
- Move cleanly beneath the squeegee
- Release from the mesh
- Leave the intended ink deposit
- Hold the required detail
- Maintain adequate opacity
- Cure according to the product instructions
How the ink prints is more important than how it feels when you push a spatula into the bucket.
Bring The Ink To Room Temperature First
Temperature has a major effect on ink viscosity. Cold plastisol can become dramatically stiffer than the same ink at normal room temperature.
If a container has been stored in a cold warehouse, delivery vehicle, garage, or loading area, allow the entire container to warm naturally before evaluating it. A five-gallon container may require considerably more time than a quart or gallon because the center of the ink remains cold after the outside of the bucket feels warmer.
Do not place the container on a heater, heating pad, flash dryer, conveyor dryer, or other direct heat source. Plastisol cures through heat. Localized heating can partially cure the ink along the bottom or sides of the container, creating hard particles or permanently thickened areas.
Move the closed container into a room-temperature production area, allow it to stabilize, and then mix it completely.
Why Plastisol Becomes Easier To Print After Mixing
Plastisol is shear-thinning. This means its apparent viscosity decreases while the ink is being stirred, mixed, or moved beneath the squeegee.
An untouched bucket may feel extremely firm. After several minutes of controlled mixing, the same ink may become smooth and creamy without adding anything to it. The ink often continues becoming easier to move as it is worked during production.
This is why adding reducer before mixing is one of the most common ink-preparation mistakes. The printer sees stiff ink, adds reducer, and then discovers that the mixture becomes much too thin after it reaches room temperature and is worked on press.
Always use mechanical or manual mixing before using chemical adjustment.
How To Mix Plastisol Ink By Hand
Small containers and small production quantities can usually be mixed with a clean, sturdy ink spatula.
Use the following process:
- Confirm that the ink has reached room temperature.
- Use a clean, dry mixing tool.
- Push the spatula to the bottom of the container.
- Lift the lower material upward and fold it into the top.
- Scrape ink from the walls and corners of the container.
- Continue until the color and texture are uniform.
- Inspect the mixture for streaks, settled pigment, lumps, or contamination.
Stirring only the top inch of the container is not enough. Pigment, specialty particles, or heavier ingredients may have settled below the surface. The entire container needs to become uniform before the ink is evaluated or portioned into a smaller bucket.
How To Mix Larger Containers
A mechanical mixer is usually more practical for gallon and five-gallon containers. Our Ink Mixing Drill Bit uses a four-way counteraction design to move ink in opposing directions and help break up settled areas. It is available in sizes for gallon and five-gallon containers.
When using a drill mixer:
- Secure the container before starting
- Insert the mixer before turning on the drill
- Begin at a slow, controlled speed
- Keep the mixer beneath the ink surface
- Move through the center, sides, and lower portion of the container
- Stop the drill before removing the mixing blade
Mixing too quickly can throw ink from the bucket and introduce excessive air. Air trapped in the ink may contribute to bubbles or inconsistencies in the printed deposit. If the ink becomes heavily aerated, allow it to rest before production.
How Long Should You Mix Ink?
There is no single mixing time that applies to every container. The required time depends on:
- Container size
- Ink temperature
- Ink formulation
- Length of storage
- Amount of settling
- Mixing equipment
Mix until the entire container is smooth and uniform. The bottom should not feel firmer than the top, and there should be no color streaks or unmixed material along the sides.
Stopping after an arbitrary number of seconds is less reliable than inspecting the ink. A small container of general-purpose color may mix quickly, while a five-gallon bucket of high-opacity white may require more time and attention.
Test The Ink Through The Actual Screen
Do not decide whether an ink is too thick based only on the container. Test it through the mesh and stencil planned for production.
A proper test should use:
- The intended screen mesh
- The production stencil thickness
- The actual squeegee or comparable blade
- The planned off-contact
- The garment or a representative test material
- Normal flood and print pressure
An ink that feels firm in the container may shear easily and clear the screen with one controlled print stroke. Another ink may feel soft but spread excessively or deposit too little color.
Evaluate the printed result for coverage, edge definition, detail, opacity, and surface quality before changing the ink.
Check The Printing Setup Before Adding Reducer
Ink is often blamed for problems caused by the screen or press setup. Before reducing the viscosity, check whether:
- The mesh count is too high for the ink
- The stencil is unnecessarily thick
- The screen tension is too low
- The off-contact is incorrect
- The squeegee edge is rounded or damaged
- The squeegee angle is too low
- The flood stroke is incomplete
- The print pressure is inconsistent
- The ink is still cold
Specialty inks containing glitter, metallic particles, reflective materials, or other large components cannot be forced through fine mesh simply by making the base thinner. The mesh opening must be large enough for the particles to pass.
Reducing the ink will not correct the wrong screen.
When Should You Use A Reducer?
Use a reducer only after the ink has reached room temperature, been thoroughly mixed, and been tested through the proper screen.
A reducer may be useful when:
- A small viscosity adjustment is needed for a higher mesh count
- The ink remains unusually difficult to clear after proper preparation
- A softer or more controlled deposit is required
- The technical instructions approve reduction for the application
Use only a reducer designed for the particular ink chemistry. Do not add water, screen wash, mineral spirits, paint thinner, household solvent, or an unidentified chemical to plastisol ink.
How To Use Visco Minus
Visco Minus is a chemical reducer designed to lower plastisol viscosity without unnecessarily harming color stability or strength. Very little is normally required.
Our recommended starting instructions are:
- Add approximately one ounce to one gallon of plastisol ink
- For small quantities, begin with only a few drops
- Do not exceed 5% of the total mixture
The 5% limit is not a target. A mixture containing that much reducer would already be extremely thin for most textile applications.
Add reducer gradually. Mix it completely, print another test, and evaluate the result before adding more. You can always add another small amount, but removing excess reducer is far more difficult.
What Happens If You Add Too Much Reducer?
Over-reducing ink can create more problems than it solves. Depending on the product and application, excessive reducer may:
- Decrease opacity
- Cause the ink to spread beyond the stencil edges
- Increase dot gain
- Reduce the intended ink deposit
- Change flash behavior
- Increase penetration into the garment
- Make the color appear weaker
- Change the finished feel
- Reduce production control
A severely over-reduced white may print easily but fail to provide the coverage the job requires. A detailed color may begin filling small negative spaces because it spreads after the screen releases.
Ink should be adjusted for printability without sacrificing the characteristics that made you select it.
Choose An Easy-Printing Ink Instead Of Over-Modifying One
Sometimes the best solution is not changing the viscosity. It is choosing an ink designed for the application.
Our 480 Series is formulated as an easy-printing general-purpose plastisol for cotton and poly/cotton garments, particularly on light fabrics or over a white underbase. It is also designed for wet-on-wet production.
For shops printing a wider variety of fabrics or trying to reduce curing temperatures, our ELT Series is a soft, stretchable, bleed-resistant plastisol designed to print easily and cure at low temperatures.
Choosing an appropriate ink series preserves more predictability than heavily reducing a product that was designed for a different mesh, fabric, or deposit.
Different Inks Should Have Different Consistencies
Do not expect every ink in the shop to have the same body.
High-Opacity Whites
White inks often have a heavier body because they contain a high pigment load and are designed to create strong coverage. They may require more complete mixing than standard colors.
General-Purpose Colors
Everyday plastisol colors are often smoother and easier to move through medium or higher mesh counts. They may feel softer than high-opacity whites while still producing durable prints.
Low-Cure And Low-Bleed Inks
These products contain ingredients selected to control curing and dye migration. Their body may differ from standard cotton inks. Do not automatically reduce them to match the feel of another series.
Process Inks
Process inks are designed for thin, controlled deposits and high mesh counts. They should flow differently from opaque spot-color inks.
Glitter And Metallic Inks
Specialty particles can settle and require thorough folding before use. These inks generally need lower mesh counts. Adding reducer will not make a large glitter flake fit through a small mesh opening.
Puff And High-Density Inks
These products depend on a controlled ink deposit to create their intended effect. Excessive reduction can weaken the height or expansion of the print.
Mixing Custom Ink Colors
When preparing a custom color, first mix each component separately so settled material does not alter the formula. Then measure the ingredients by weight rather than estimating by volume or appearance.
A repeatable process is:
- Bring every component to room temperature.
- Mix each original container until uniform.
- Place a clean container on a digital scale.
- Tare the scale to zero.
- Add each component according to the formula.
- Mix the combined color thoroughly.
- Print and cure a test sample.
- Record all measured adjustments.
If a pigment mixing system is being used, remember that concentrated pigment is not printable ink by itself. It must be combined with the proper base. The base supplies the viscosity, curing, stretch, opacity, and other performance characteristics of the finished ink.
Evaluate Custom Colors After Curing
Wet ink is not the final color. Always print and cure a sample before deciding whether a mixture is correct.
The finished appearance can be affected by:
- The garment color
- The white underbase
- The mesh count
- The number of print strokes
- The thickness of the ink deposit
- The curing process
- The lighting used during evaluation
A color that looks correct on the mixing spatula may become lighter, darker, warmer, or cooler after printing. Approve the color under the same conditions that will be used for production.
Preparing Water-Based Ink
Water-based ink also requires mixing, but it should be handled according to the instructions for that particular system.
Water-based products can lose moisture while the container is open. Do not automatically replace that moisture with water unless the manufacturer specifically approves the amount and method. Too much added water can reduce color strength, alter viscosity, and affect curing or wash durability.
Keep containers closed when not in use, mix gently enough to avoid excessive foam, and use only approved additives. Activated water-based or discharge inks may have a limited working time after the activator is added.
Never apply plastisol mixing instructions or reducers to a water-based ink system.
Keep Mixing Tools Clean
Clean tools are essential for consistency. A trace of black ink can dull a pale yellow. Cleaner residue or water can change plastisol viscosity and printing behavior.
Use separate or thoroughly cleaned tools when moving between:
- Light and dark colors
- Standard and specialty inks
- Plastisol and water-based systems
- Printable inks and concentrated pigments
Make sure containers are clean and dry before transferring ink. Do not return contaminated ink from a screen to the original bucket.
Maintain Consistency During Production
Ink preparation does not end when the first shirt is printed. Heat, repeated flashing, garment fibers, and press conditions can change the way ink behaves during a long run.
To keep the ink consistent:
- Add manageable quantities to the screen
- Keep the image area flooded when appropriate
- Prevent the screen from becoming excessively hot
- Stir the ink periodically if settling occurs
- Remove lint and contamination
- Use the same flood and print technique throughout the run
- Keep additional ink covered until it is needed
Ink sitting on a hot screen may become noticeably softer. Do not add reducer merely because the ink behaves differently after the press becomes warm. First identify whether screen temperature is changing the process.
Document Every Adjustment
If reducer, pigment, base, or another approved additive is placed into an ink container, record it.
The label or production record should include:
- Product and color
- Original quantity
- Additive used
- Amount added
- Date of adjustment
- Person who made the adjustment
- Job or garment for which it was prepared
Without that information, another printer may add more reducer to an ink that has already been modified. Documentation also makes a successful production setup easier to reproduce.
Common Ink Mixing Mistakes
Most ink-consistency problems come from a few repeated mistakes:
- Evaluating cold ink
- Mixing only the top of the container
- Adding reducer before testing the ink
- Using an incompatible additive
- Mixing at excessive speed
- Introducing contamination from dirty tools
- Trying to force specialty particles through fine mesh
- Failing to record adjustments
- Assuming every ink should have the same viscosity
Following the proper preparation sequence prevents most of these problems.
Troubleshooting Ink That Seems Too Thick
If an ink seems too thick:
- Confirm that it is at room temperature.
- Mix it completely from the bottom upward.
- Check for partially cured particles or contamination.
- Verify that the mesh is appropriate for the ink.
- Inspect screen tension and stencil thickness.
- Inspect the squeegee edge and press setup.
- Run a controlled print test.
- Add a very small amount of approved reducer only if necessary.
If hard or rubbery particles remain after mixing, the ink may have been partially cured by heat. Reducer will not restore cured plastisol.
Troubleshooting Ink That Seems Too Thin
If an ink is spreading, penetrating the fabric excessively, or losing opacity:
- Check whether too much reducer was added
- Confirm that water or cleaner did not enter the container
- Make sure the screen is not becoming unusually hot
- Verify that the correct ink series is being used
- Check whether another thinner ink was mixed into the container
- Reduce unnecessary squeegee pressure
Depending on the system, adding more unmodified ink may help restore the mixture. Measure and document the correction so the final ratio is known.
Ink Preparation Checklist
- Store ink at normal room temperature
- Never warm plastisol on a heater or curing device
- Use clean, dry tools and containers
- Mix from the bottom and scrape the sides
- Use a controlled speed with mechanical mixers
- Allow excessive air bubbles to settle
- Test through the actual production screen
- Check the press setup before changing the ink
- Use only approved reducers and additives
- Add reducer in very small measured amounts
- Evaluate the cured print rather than wet ink
- Record every adjustment
Final Thoughts
Getting the right screen printing ink consistency is usually a matter of proper preparation rather than chemical modification. Cold, settled plastisol can feel much thicker than it will after reaching room temperature and being mixed thoroughly.
Begin by bringing the ink to room temperature. Mix the entire container, including the bottom and sides. Test it with the actual mesh, stencil, squeegee, and garment. Check the press setup before assuming the ink needs to be thinner.
When an adjustment is genuinely required, use a compatible reducer such as Visco Minus, add only a small measured amount, and test again. More reducer is not automatically better.
The proper consistency is the one that allows the ink to flood, print, release, cover, and cure as intended. By controlling temperature, mixing method, additives, and production settings, you can achieve smoother prints without sacrificing opacity, color strength, or durability.